DAWNICE
14 years of production experience

To Strive Forward No Energy Waste

Leave Your Message
Dawnice HZEB-HCT-125/522: 522kWh All-in-One Energy Storage System by China Suppliers and Factory
Hot Products

Dawnice HZEB-HCT-125/522: 522kWh All-in-One Energy Storage System by China Suppliers and Factory

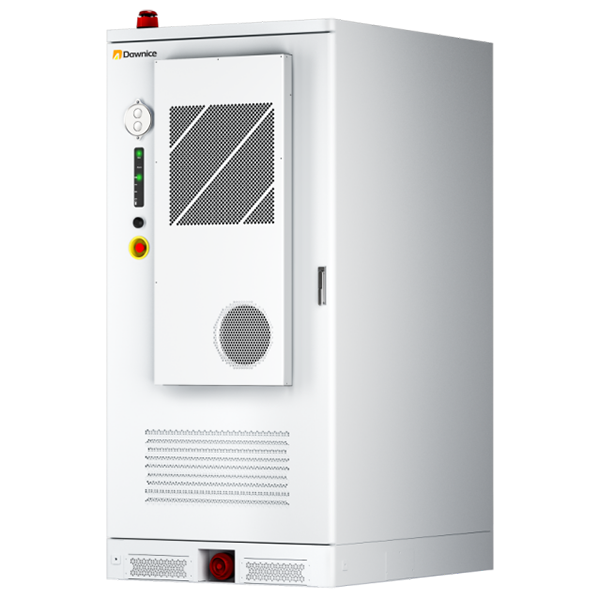
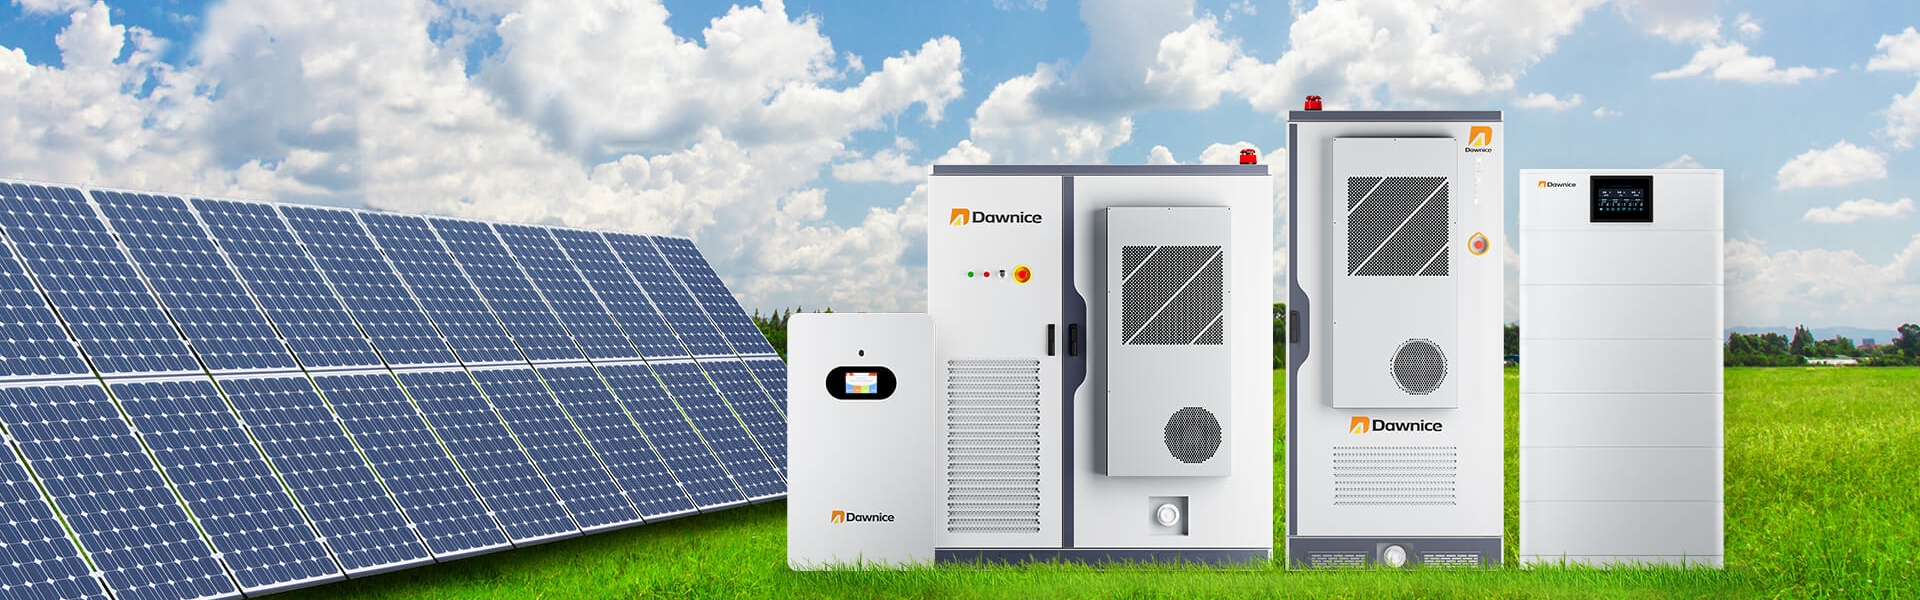
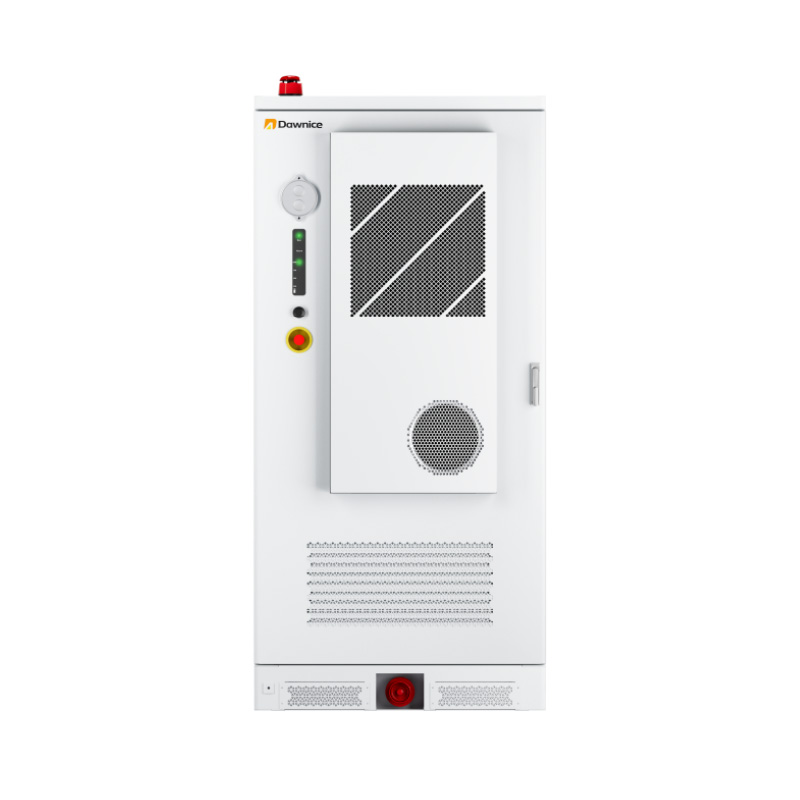
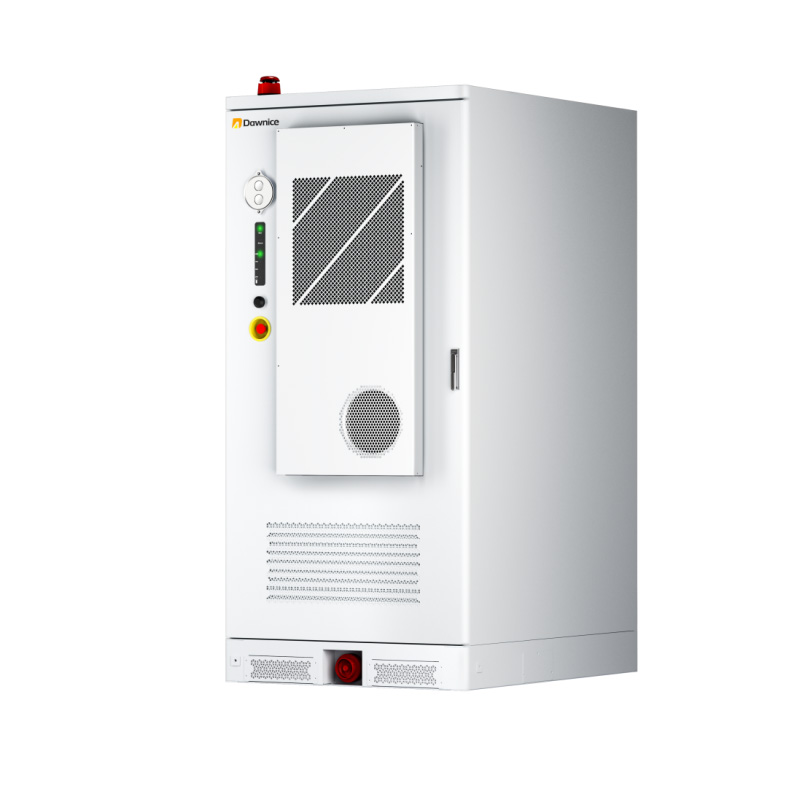
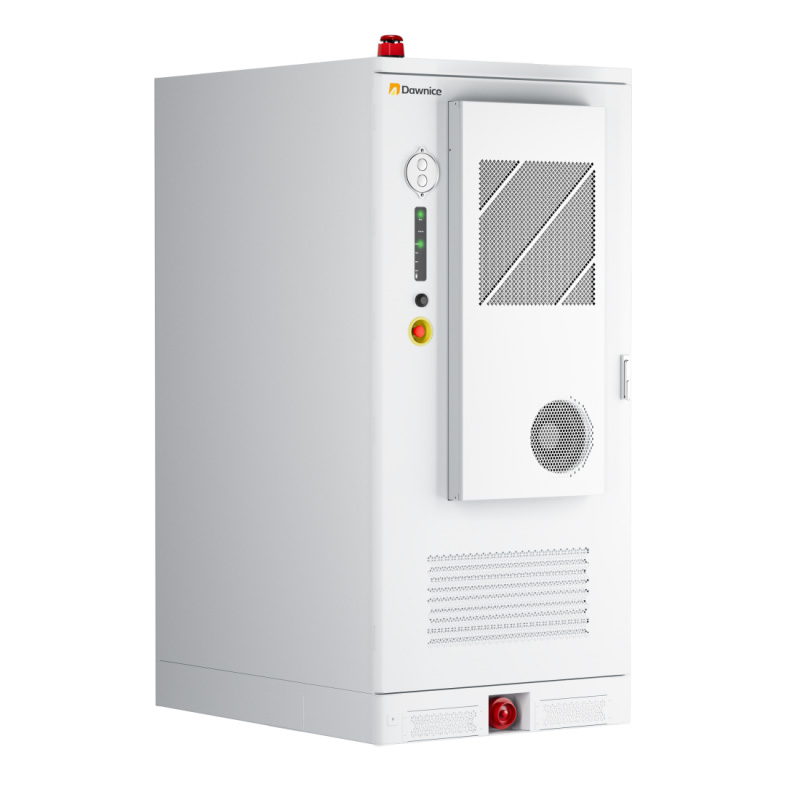
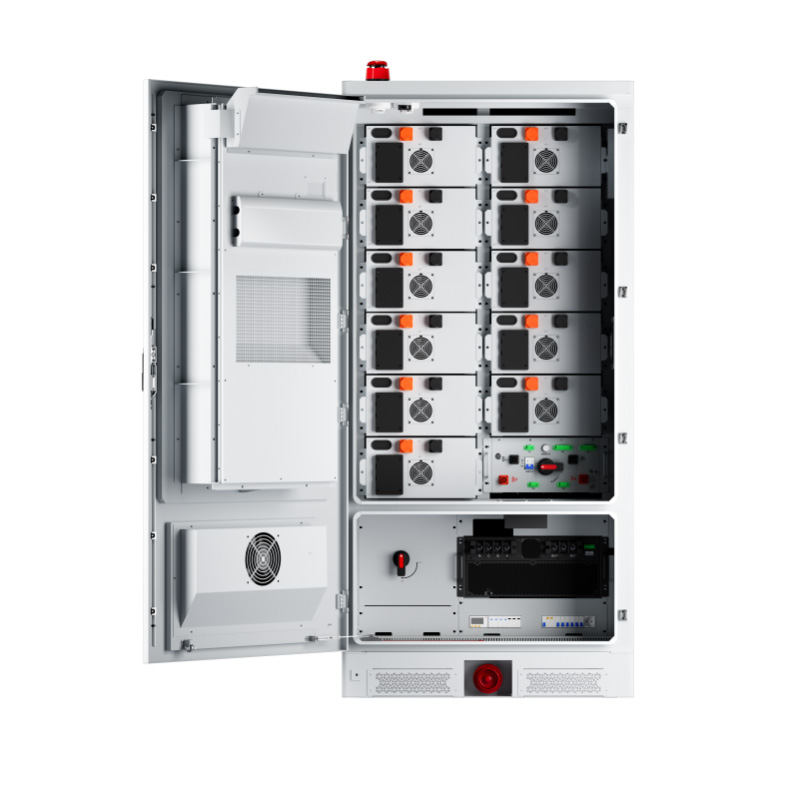
The Dawnice HZEB-HCT-125/522 is a state-of-the-art energy storage system with a capacity of 522kWh, designed specifically for commercial and industrial grid-connected applications. Manufactured in China, this high-capacity system boasts a 125kW rated AC power output (230/400VAC, 3W+N+PE), ensuring efficient and stable support for your energy grid. Utilizing advanced LiFePO₄ battery technology arranged in a 2P260S configuration, it offers an exceptional battery life of up to 8000 cycles at 90% DOD under optimal conditions of 25°C. With a power factor of 0.99 and a current distortion rate below 2%, this system guarantees reliable performance across various environments. Additionally, it features IP54 protection, integrated aerosol fire protection, air cooling, and MODBUS TCP/RTU communication capabilities, making it a complete, turnkey solution from top suppliers in the industry for large-scale energy storage needs. Choose the Dawnice HZEB-HCT-125/522 for unmatched efficiency and reliability from a trusted factory.

    High-Capacity All-in-One Design – 522kWh Reliable Storage

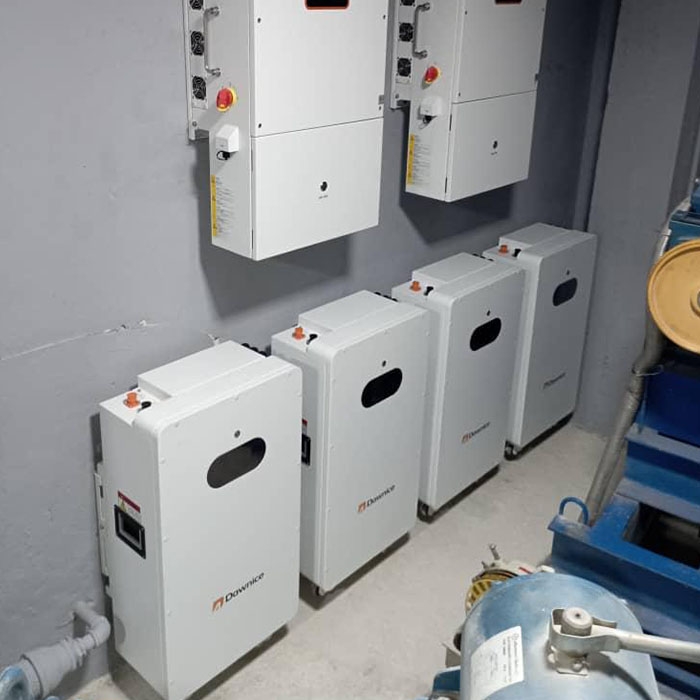
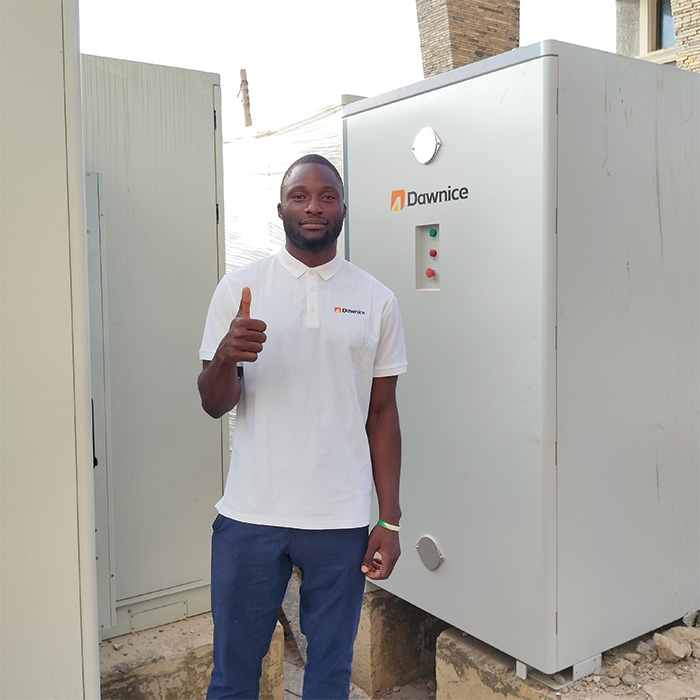
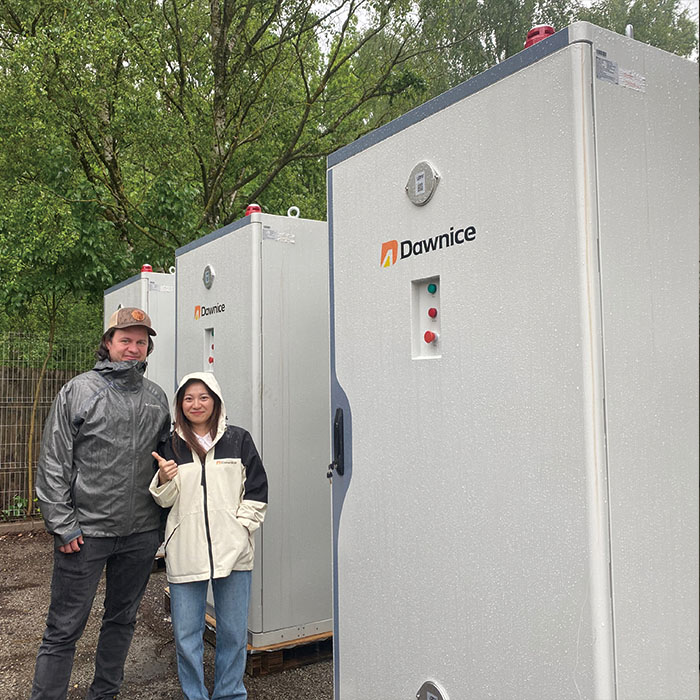
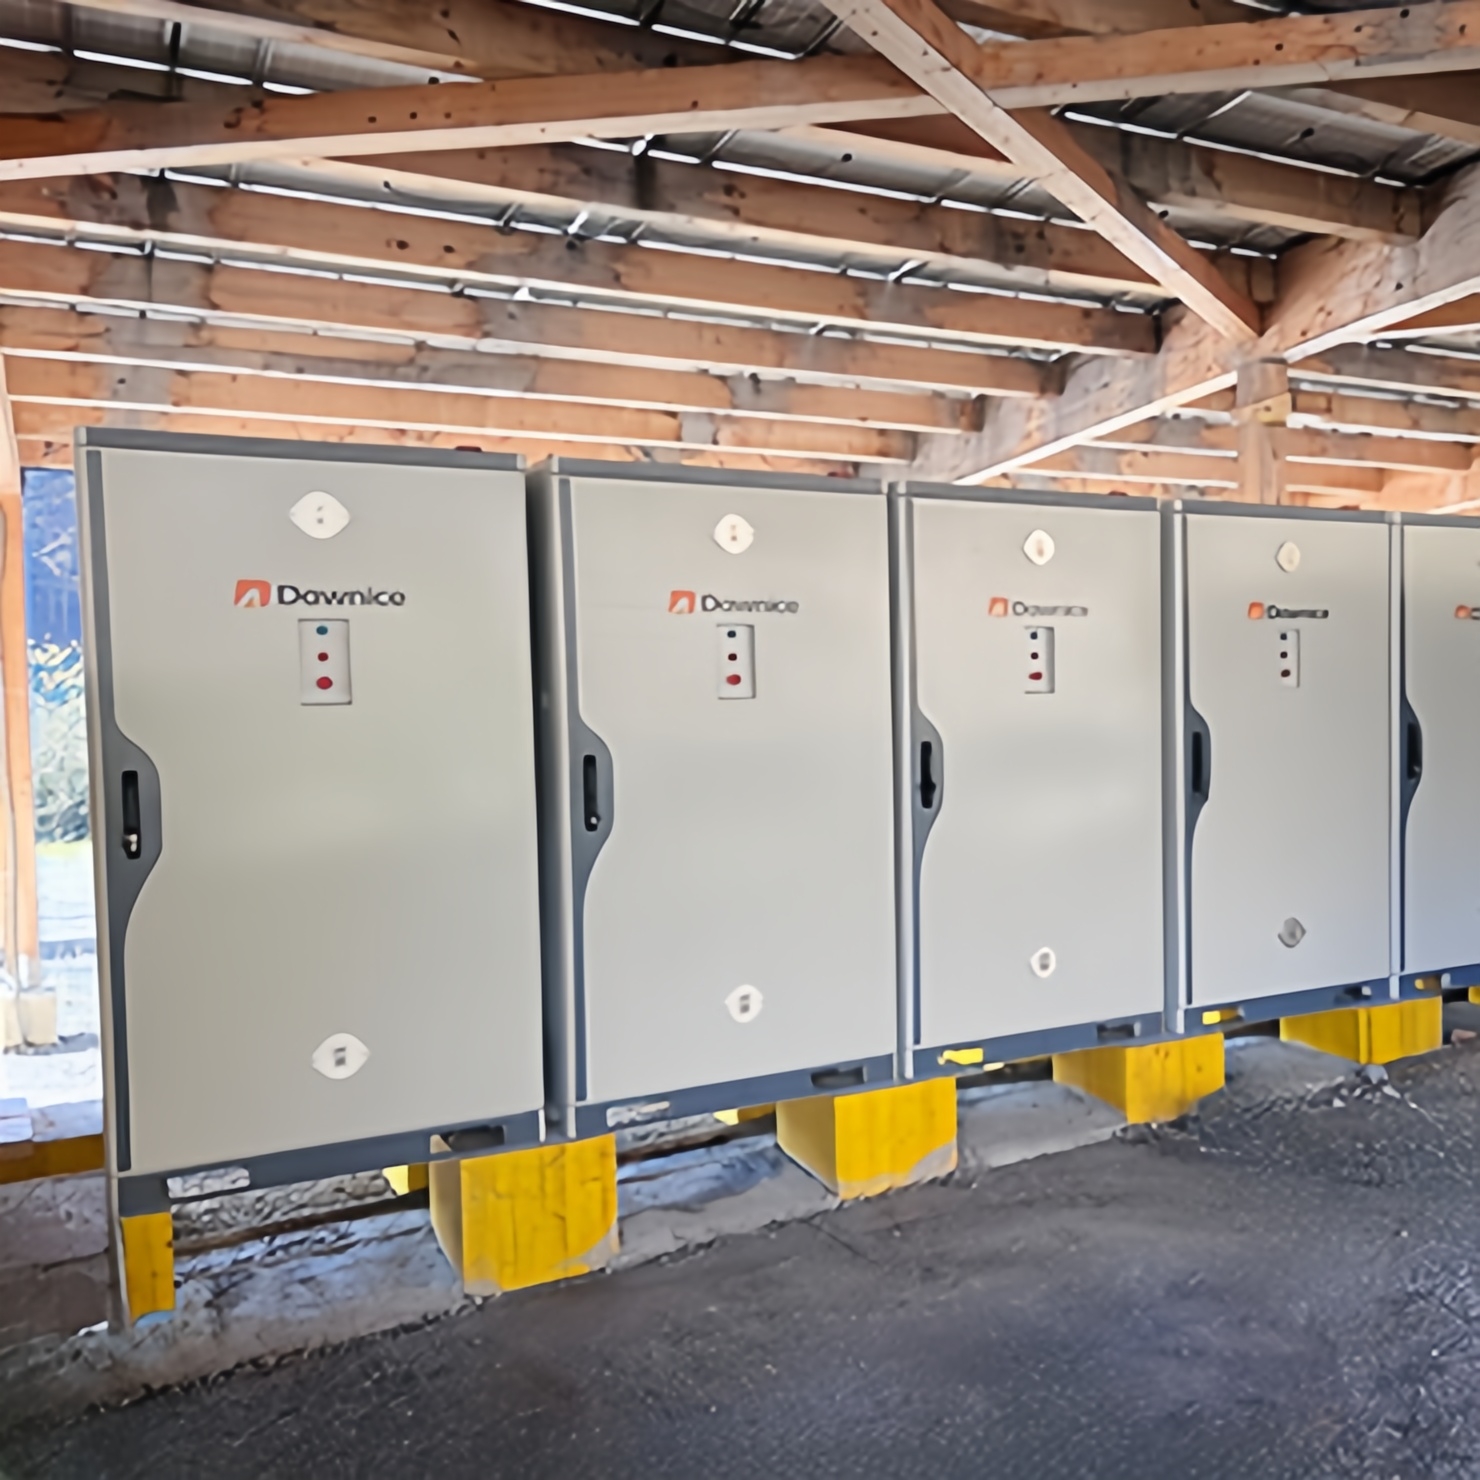
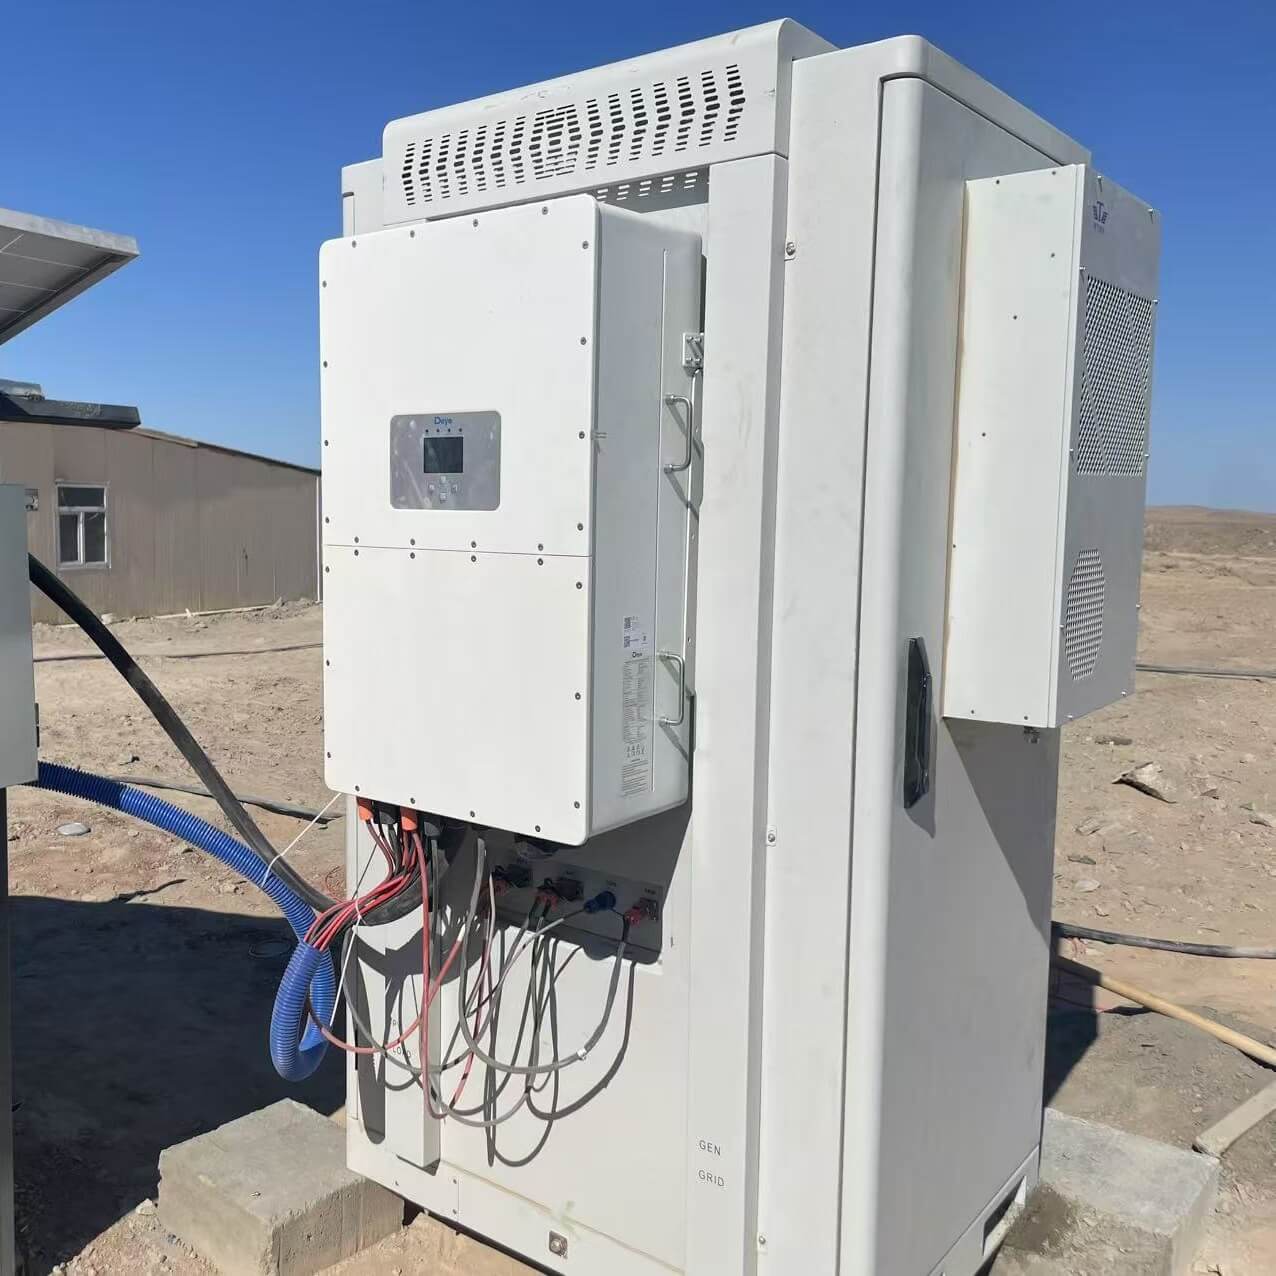
    The Dawnice HZEB-HCT-125/522 integrates 125kW rated AC power and 522kWh battery capacity into a single, comprehensive enclosure. Its 3W+N+PE output type (230/400VAC) with 50/60Hz grid frequency compatibility ensures seamless grid connection for commercial and industrial applications.

    System specifications:
    Battery Configuration

    2P260S LiFePO₄

    Nominal Voltage

    832VDC

    Voltage Range

    728–936VDC

    Max Charge/Discharge Multiplier

    0.5P

    Cycle Life

    ≥8000 cycles (@25°C, 0.5P, 90% DOD, 70% EOL)

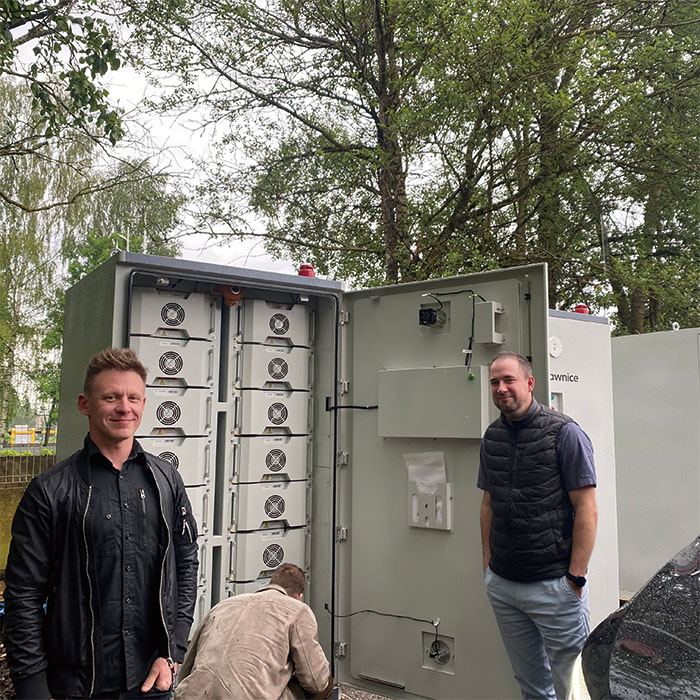
    The all-in-one cabinet design simplifies installation and reduces on-site commissioning time, making it an ideal turnkey solution for factories, commercial buildings, and utility-scale projects requiring stable, high-capacity energy storage.

    Grid-Connected Excellence with High Power Quality

    Engineered for superior grid interaction, the HZEB-HCT-125/522 delivers exceptional power quality with:

    Power Factor

    0.99 (adjustable range from 1 leading to 1 lagging)

    Current Distortion Rate

    <2% – ensuring clean power injection to the grid

    Rated AC Power

    125kW continuous grid-connected output

    This high-performance grid-tied capability enables:
    • Peak shaving and load shifting for electricity cost reduction
    • Grid frequency regulation and voltage support
    • Renewable energy integration and smoothing
    • Demand charge management for C&I users

    The system's advanced inverter technology ensures stable operation and compliance with stringent grid connection requirements worldwide.

    Comprehensive Safety and Environmental Protection

    Safety is paramount in the HZEB-HCT-125/522 design, featuring multiple layers of protection:

    Physical Protection
    IP54 Rating: Dust-protected and splash-resistant for indoor/outdoor installation.
    Robust Cabinet Dimensions: 2500x2250x2300mm with 5980kg weight for stability.
    Active Safety Systems
    Aerosol Fire Protection: Integrated suppression system for battery thermal events.
    Air Cooling Method: Efficient thermal management without complex liquid cooling infrastructure.
    Operating Temperature Range: -30°C to 55°C – suitable for extreme climates.
    Altitude Capability: ≤2000m standard operation.
    Monitoring and Control
    Communication: Dual MODBUS TCP/RTU protocols for SCADA integration.
    Real-time BMS: Continuous monitoring of voltage, current, temperature across all cells.
    Remote Diagnostics: Remote diagnostics and firmware upgrade capability.

    With relative humidity tolerance <90% and noise level ≤75dB (≤1m) , the system maintains comfortable operation even in sensitive environments.

    Industrial-Grade Reliability for Long-Term Investment

    The HZEB-HCT-125/522 is built for decades of service with:
    • 8000-cycle lifetime at 90% DOD (70% EOL threshold)
    • 0.5P charge/discharge capability for balanced performance and longevity
    • LiFePO₄ chemistry – inherently safe with no thermal runaway risk
    • Proven cell configuration (2P260S) for consistent performance across the bank
    Ideal applications:

    ● Commercial & industrial peak shaving

    ● Renewable energy firming (solar/wind integration)

    ● Grid ancillary services

    ● Backup power for critical infrastructure

    ● Microgrid and utility-scale storage projects

    Global Quality with Local Technical Support

    Trusted by customers in over 160 countries, Dawnice brings decades of energy storage expertise to every installation. The HZEB-HCT-125/522 is manufactured under strict quality control and certified to international standards.

    Why choose Dawnice for your C&I project:
    • Turnkey solution – fully integrated and tested before shipment
    • Modular scalability – multiple units can be paralleled for larger projects
    • Global commissioning support available
    • Comprehensive warranty and long-term service agreements
    • Remote monitoring via MODBUS TCP/RTU for easy integration with existing systems

    With our expanding global footprint, including upcoming support hubs in key markets, Dawnice ensures you receive not just world-class products, but also responsive local assistance throughout your project lifecycle.

    Frequently Asked Questions (FAQ)

    What are the power and capacity ratings of the HZEB-HCT-125/522?
    The system delivers a rated AC power output of 125kW and provides a total battery capacity of 522kWh in an all-in-one enclosure.
    What is the battery chemistry and expected cycle life?
    The unit utilizes safe, high-performance LiFePO₄ (Lithium Iron Phosphate) chemistry in a 2P260S configuration, delivering a cycle life of ≥8000 cycles (@25°C, 0.5P, 90% DOD, 70% EOL).
    What fire suppression and thermal safety systems are integrated?
    The system is equipped with an integrated aerosol fire suppression system, air cooling thermal management, and real-time BMS cell monitoring.
    What environmental conditions can the cabinet withstand?
    Featuring an IP54-rated enclosure, it operates across temperatures from -30°C to 55°C, handles relative humidity up to <90%, and supports operational altitudes of ≤2000m.
    Which communication protocols are supported for SCADA and remote monitoring?
    It supports dual MODBUS TCP/RTU protocols for seamless SCADA integration, comprehensive remote diagnostics, and firmware upgrades.
    Can multiple units be paralleled for larger projects?
    Yes, the system offers modular scalability, allowing multiple units to be paralleled for large commercial, industrial, microgrid, or utility-scale installations.